TL;DR
Among the 2026 manufacturing industry trends, fund connected factory data first if plant data is scattered, and industrial AI first if it is already clean. The eight shifts are industrial AI, connected data, flexible automation, supply chain resilience, workforce skills, energy and circular production, additive manufacturing and servitization. Cost pressure is real, since 83.1% of manufacturers in the NAM Q2 2026 survey named raw material costs a top challenge. Investment keeps flowing anyway, because Deloitte found 78% of large US manufacturers put more than 20% of their improvement budget into smart manufacturing. Robotics, additive, digital twins and connected services pay off once that data foundation exists, so they usually come second. Pick one plant problem, prove one KPI in 90 days, then scale what worked.
Key Takeaways
- Eight manufacturing industry trends shape 2026: industrial AI, connected factory data, flexible automation, supply chain resilience, workforce skills, energy and circular production, additive manufacturing and servitization.
- Cost and trade pressure set the pace, with raw material costs and trade uncertainty topping the NAM Q2 2026 list of challenges.
- Connected factory data comes first for most plants, because predictive maintenance, AI inspection, digital twins and connected services all read from it.
- Robot installations reached 542,000 in 2024, and the IFR forecasts more than 700,000 a year by 2028.
- People stay central, with Deloitte expecting more than 81% of task hours to remain human-driven.
- Fund the trend whose data you already have and whose KPI you already measure, then prove it in a 90-day pilot.
The Monday Report That Takes Two Days
Picture a plant manager at a mid-sized auto parts supplier at 7 a.m. on a Monday. The leadership review starts at ten, and last week’s scrap numbers still do not agree.
First, downtime sits in the machine historian. Defects sit in the quality system, while orders and costs live in the ERP. So two analysts spend the morning pasting exports into a spreadsheet. By the time the numbers line up, the line has already run another shift with the same defect.
Still, that plant is not short of technology. It has sensors, a manufacturing execution system (MES) and a capable ERP. What it lacks is one connected view of production, and that gap decides which manufacturing industry trends can help it soon. Our manufacturing technology trends infographic shows which of those trends are gaining ground in 2026.
This guide explains the eight shifts shaping US plants in 2026 and the data each one needs. It then gives you a simple way to decide which one to fund first.
Why Manufacturing Industry Trends Look Different in 2026
Manufacturers are investing in 2026 under steady cost pressure, and that pressure changes which trends deserve money first. Projects now need a short payback and a clear owner, so a slide about the factory of the future no longer wins a budget.
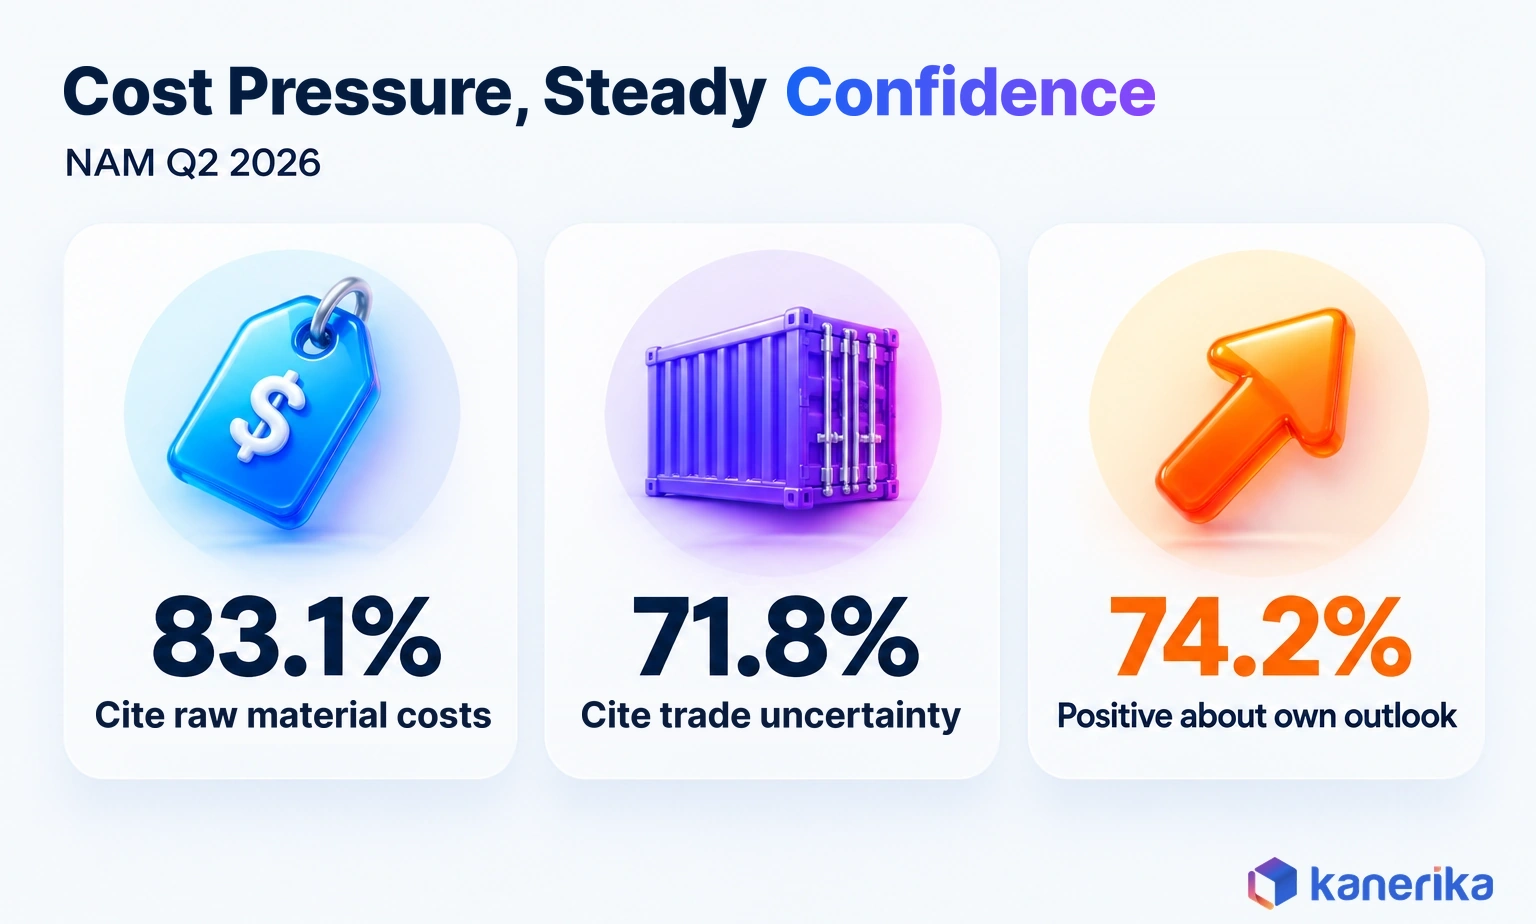
The National Association of Manufacturers shows the mood clearly. In its Q2 2026 Manufacturers’ Outlook Survey, fielded May 12 to 28 with 215 responses, 74.2% of respondents felt positive about their own company’s outlook. That was slightly lower than the 75.3% recorded in the first quarter.
The same survey also shows where the strain sits. Increased raw material costs were a top challenge for 83.1% of respondents, while 71.8% cited trade uncertainties.
Spending on plant technology has still held up. Deloitte’s 2025 Smart Manufacturing survey polled 600 executives at US companies with at least $500 million in revenue. It found that 78% allocate more than 20% of their improvement budget to smart manufacturing. Respondents reported gains of up to 20% in production output, 20% in employee productivity and 15% in available capacity.
Policy and new demand also add a push. Deloitte’s 2026 manufacturing industry outlook links much of the new investment to incentives, data center build-outs and semiconductors. According to Deloitte, the One Big Beautiful Bill Act also raised the advanced manufacturing investment credit from 25% to 35%.
Put together, the numbers point to a practical rule. A plant that cannot see its own costs, scrap and downtime in one place will struggle to prove any of the gains above. That is why the data foundation keeps showing up as the first step in the trends below.
The 8 Manufacturing Industry Trends at a Glance
Each of the eight manufacturing industry trends solves a specific plant problem. Each one also depends on data that a plant may or may not collect yet, so the table lines them up on the same terms.
The maturity column is our read of where most mid-sized and large US plants sit. “Scaling” means many plants run it in production, and “early” means real deployments exist but are uneven. “Pilot” means most plants are still testing.
| Trend | Plant problem it solves | Data it needs | Maturity | First KPI |
|---|---|---|---|---|
| 1. Industrial AI | Unplanned stops and escaped defects | Sensor history, work orders, labeled defect images | Scaling | Unplanned downtime hours |
| 2. Connected factory data and IT/OT convergence | Reports that take days and never agree | PLC, historian, MES and ERP data in one model | Scaling | Time to publish the weekly plant report |
| 3. Flexible automation | Hard-to-fill repetitive roles | Cycle times, station layouts, safety zones | Early | Units per labor hour |
| 4. Supply chain resilience | Shortages and tariff cost swings | Supplier, bill of materials, order and lead-time data | Early | Supplier on-time delivery |
| 5. Workforce transformation | Skills gaps and slow onboarding | Training records, skills matrix, work instructions | Early | Time to competency for new hires |
| 6. Energy and circular production | Rising energy bills and scrap | Meter data by line, scrap and rework records | Early | Energy per unit produced |
| 7. Additive manufacturing | Long waits for tooling and spares | CAD files, part demand, lead times | Pilot | Lead time for tooling and spares |
| 8. Servitization | Flat equipment margins | Field data from installed products, service history | Pilot | Service share of revenue |
Read the data column before the maturity column. A trend that is scaling elsewhere can still be a pilot in your plant if the data is missing. AI inspection, for example, needs labeled defect images that many lines have never stored.
1. Industrial AI Moves From Pilots to Production Lines
Industrial AI in 2026 means models that run inside daily plant work, rather than demos that live in an innovation lab. The shift is less about new algorithms and more about wiring models into the systems where maintenance, quality and planning decisions already happen.
Consider a packaging line that stops twice a week for jams. A model that predicts jams helps only if its alert reaches the shift lead, opens a work order and records whether the fix worked. When that loop closes, the model improves each month. When it does not, the pilot quietly ends.
Gains like the ones Deloitte’s respondents reported depend on that loop closing. Three uses carry most of that value on the floor, and each one has a different data need.
Kanerika Service
AI and Machine Learning Services
Kanerika builds and runs AI models for plant operations, from predictive maintenance and quality inspection to forecasting, on governed enterprise data.
Explore AI ServicesPredictive maintenance on critical assets
Predictive maintenance uses vibration, temperature, pressure and motor current readings to spot a failure before it stops the line. Sensor data alone is not enough, though. The model also needs work-order history from the maintenance system, so it can learn which patterns came before a real failure.
Start with the two or three assets whose failure halts the whole line, such as a main press, a filler or a compressor. Then track unplanned downtime hours and mean time between failures on those assets. Our guide to AI in predictive maintenance covers model choices and sensor setup in detail.
AI visual inspection for quality
Camera-based inspection catches surface defects, missing parts and label errors at line speed, especially late in a shift when human checks get tired. The hard part, though, is the training data. A model needs thousands of labeled images of good and bad parts, taken under the lighting the line really has.
Measure it with first-pass yield and escaped defects, which are the faults a customer finds. The guide to AI in quality assurance explains how labeling, thresholds and human review fit together.
GenAI copilots and AI agents for technicians and planners
Generative AI copilots answer questions from manuals, past work orders and standard operating procedures. A technician facing an unfamiliar fault can ask what fixed it last time, instead of calling the one engineer who remembers. Planners also use similar tools to draft schedules and summarize shift handovers. Our guide to generative AI in manufacturing covers more copilot use cases.
AI agents go a step further, since they can act within set limits, for example by raising a purchase request or moving a job. Deloitte’s 2026 outlook names agentic AI as part of the next phase of smart manufacturing. For use cases, autonomy levels and controls, see our guide to agentic AI in manufacturing. Delivery support sits with Kanerika’s AI and ML services.
2. Connected Factory Data and IT/OT Convergence
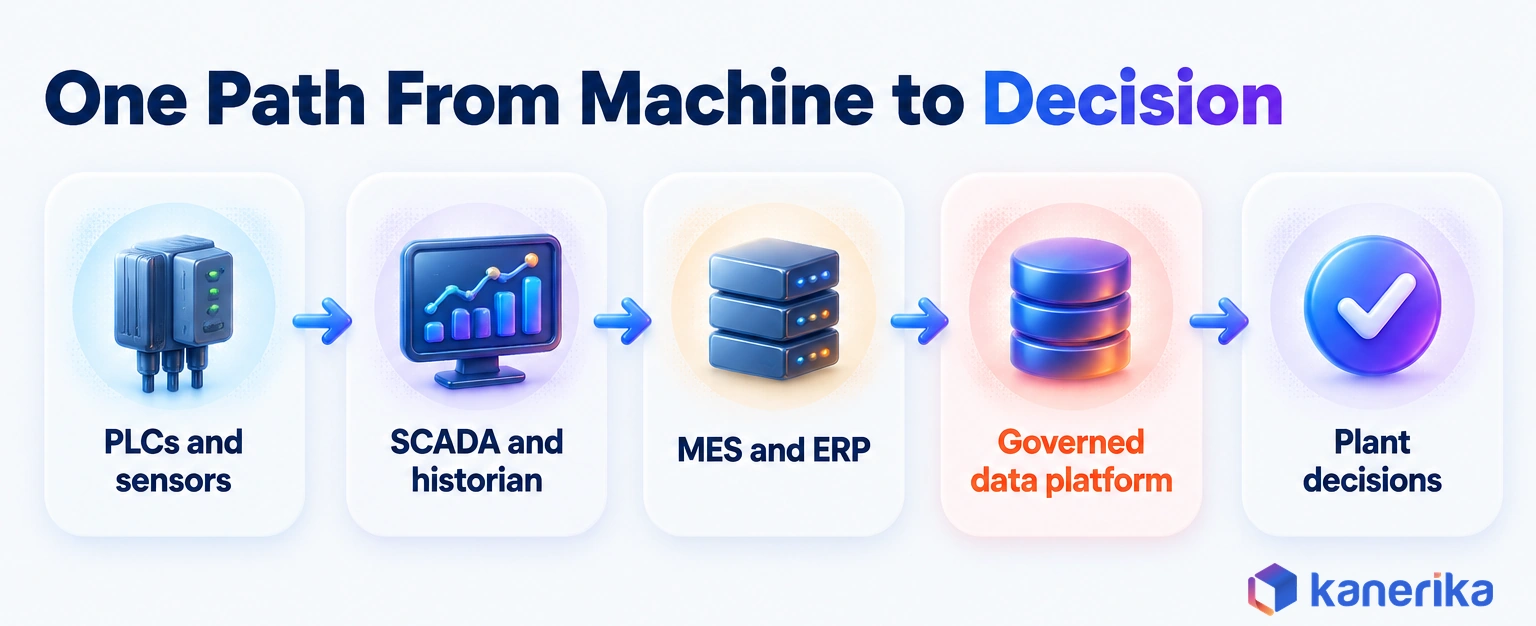
IT/OT convergence means the operational technology on the floor and the business systems in the office finally share the same production context. Operational technology (OT) covers PLCs, sensors and SCADA, while IT covers the MES, ERP and quality systems.
More sensors alone rarely fix a plant’s visibility problem, though. A downtime event is useful only when you also know which order, product, shift and crew it hit. That context sits in other systems, so the real work is joining them.
A shared reference model helps here. The ISA-95 standard, adopted internationally as IEC 62264, covers how business and logistics systems integrate with manufacturing control systems. Mapping each system to its levels keeps data joins consistent from plant to plant.
In practice, plant data moves along one path. PLCs and sensors feed SCADA and a historian, which time-stamps every reading. The MES and ERP then add orders, materials and costs. Finally, a governed data platform joins all of it under shared definitions, and plant teams make decisions from that single model.
The payoff shows up first in reporting speed. When a plant manager no longer waits for analysts to reconcile exports, problems get fixed within the shift instead of the following week. The FoodPharma project described in the Kanerika section below shows how large that gap can be.
Two common analytics jobs sit on top of this foundation. Manufacturing analytics explains performance on the line, while business intelligence for manufacturing puts plant and financial results in front of managers. Both depend on the same data integration work underneath.
Digital twins move from demo to planning tool
A digital twin is a live model of a physical asset, line or process that updates from plant data. An asset twin mirrors one machine, such as a press. A line twin models how stations interact, so planners can test a new product mix before changing the real line. A process twin goes wider and follows material and energy across a whole plant.
All three run on the connected data described above. A twin fed by stale or partial data simply makes confident mistakes faster. So plants that build the data path first find twins far cheaper to add later. Our guide to AI-powered digital twins covers the build options.
Checklist
Data Integration Checklist
Check your sources, pipelines, data quality and ownership before you connect historian, MES and ERP data into one platform.
Get the Checklist →3. Flexible Automation: Cobots, AMRs and Physical AI
Flexible automation means robots that can be moved, retaught and shared across jobs, rather than fixed cells built for one product. It matters because product mixes now change faster than old automation projects could pay back.
Adoption numbers also keep climbing. The World Robotics 2025 report from the International Federation of Robotics, released on September 25, 2025, counted 542,000 industrial robots installed in 2024. That was more than double the figure ten years earlier, and the fourth straight year above 500,000. The IFR forecasts 575,000 installations in 2025, a 6% rise, and more than 700,000 a year by 2028.
Collaborative robots, or cobots, can work beside people without full safety cages when a risk assessment allows it. Autonomous mobile robots (AMRs) carry material between cells and stores without fixed tracks. Together they suit tasks such as these:
- Machine tending, such as loading and unloading CNC machines across shifts.
- Palletizing and case packing at the end of the line.
- Repetitive assembly steps such as screwdriving, gluing or fastening.
- Moving work in progress between stations, which AMRs handle without conveyors.
OSHA notes that many robot accidents happen during non-routine work such as programming and maintenance, and it has no standard written for robotics alone. So the risk assessment carries the weight, on the line and in the warehouse, which our guide to AI in warehouse management covers for AMRs.
Physical AI is the next step, with robots that perceive and adapt to their surroundings instead of following fixed paths. A Manufacturing Leadership Council survey from early 2025, as cited by Deloitte, put the share of manufacturers planning to use physical AI within two years at 22%. At the time of the survey, only 9% used it. Our guide to AI in robotics covers use cases and safety standards in more depth.
4. Supply Chain Resilience, Tariffs and Regional Sourcing
Supply chain resilience is the ability to keep plants running and margins intact when a supplier, a port or a tariff changes without warning. It is a board topic in 2026 because input costs and trade rules keep moving at the same time.
The NAM figures quoted earlier, 83.1% for raw material costs and 71.8% for trade uncertainty, describe a planning problem as much as a cost problem. A tariff change on one imported component can alter the cost of hundreds of finished products. A plant that cannot trace that component through its bills of material will find out from the next margin report.
Resilient manufacturers work through four steps, and several gain from intelligent automation in supply chain:
- Map tier-one suppliers and the critical tier-two suppliers behind them, with lead times and country of origin.
- Dual-source the parts that have a single point of failure, starting with those that stop a line.
- Model tariff and price scenarios against the bill of materials, so finance sees the exposure before it lands.
- Use demand sensing, which reads recent orders and customer signals, to adjust production plans weekly instead of quarterly.
Better forecasts make every one of those steps cheaper. ABX, a flexible-packaging maker with eight US facilities, reached 85% accurate sales forecasts after Kanerika built AI-driven forecasting on its data. The same work raised its ability to identify churn risk by 50%.
Case Study
85% Accurate Sales Forecasts for a Packaging Manufacturer
ABX, a flexible-packaging maker with eight US facilities, reached 85% accurate sales forecasts and a 50% increase in identifying churn risk with AI-driven forecasting from Kanerika.
Read the Case Study →Planning also extends past the plant gate. Teams that want analytics across freight and warehouse operations can start from the same data model. Automotive suppliers face sharper versions of these pressures, which our guide to data analytics in the automotive industry covers. Once planners want to automate parts of the work, see the guide to AI agents in supply chain planning.
5. Workforce Transformation and the Skills Gap
Workforce transformation means changing how plants hire, train and support people, because technology pays off only when skilled operators can run it. The skills gap is the hardest limit on many of the other seven trends.
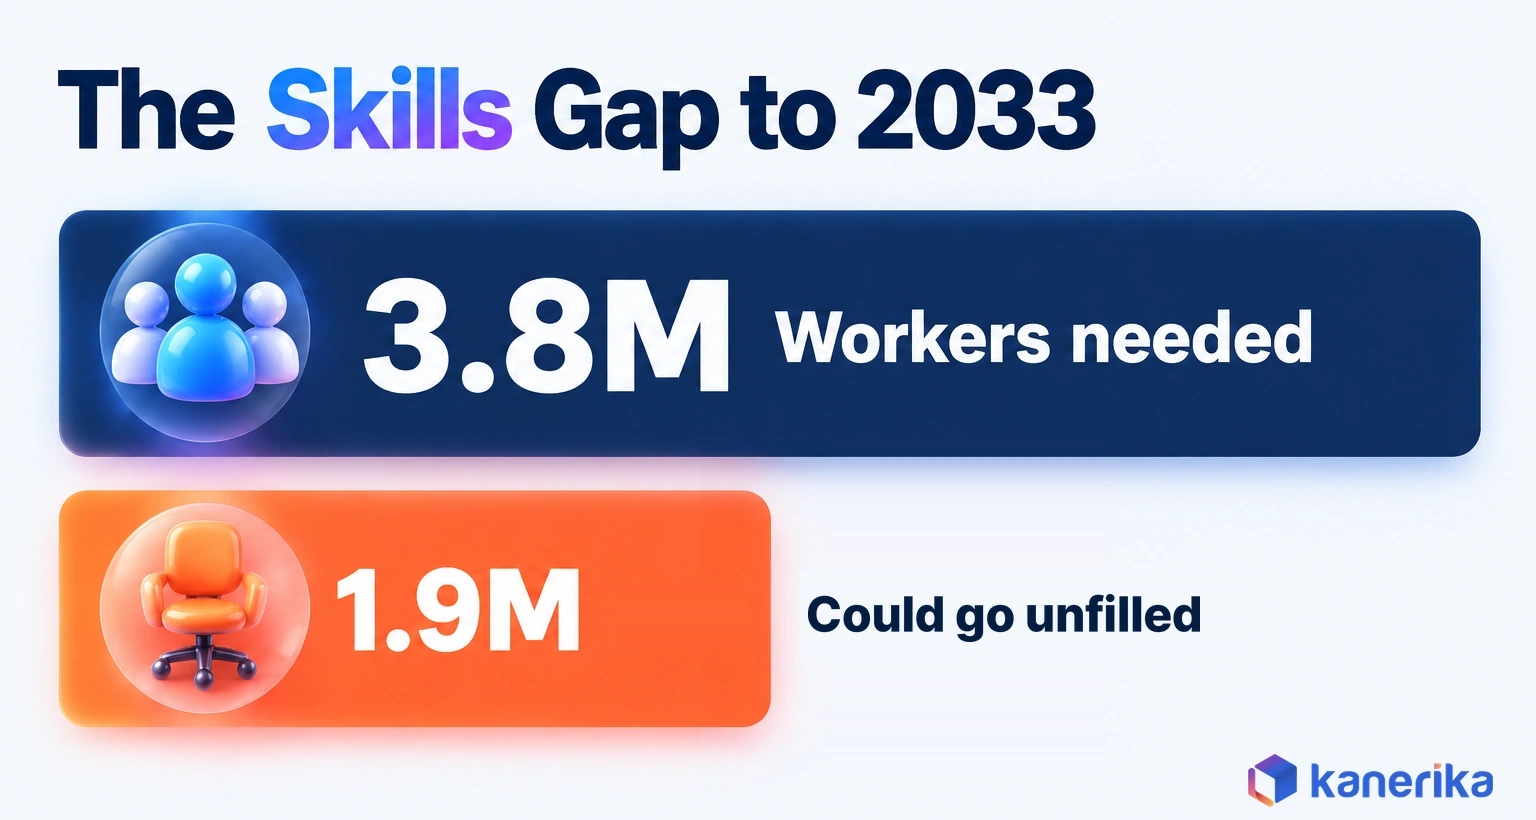
The numbers are large. A study by The Manufacturing Institute and Deloitte estimated that US manufacturers may need up to 3.8 million new workers between 2024 and 2033. As many as 1.9 million of those jobs could go unfilled.
Automation, however, does not remove the need for people. Deloitte’s 2026 outlook expects more than 81% of task hours to remain human-driven. So the practical aim is to make each worker more capable, not to empty the floor.
Plants are responding in three ways. Some write digital work instructions that show each step at the station. Others pair new hires with copilots that answer questions from manuals and past fixes. A smaller group uses extended reality (XR) headsets to train people on rare or risky tasks without stopping a live line.
Design matters as well. Systems that keep an operator in the loop earn trust faster than systems that act alone, especially when the operator can override a bad recommendation. Time to competency for new hires is a good first KPI.
6. Energy Efficiency, Sustainability and Circular Production
Sustainable manufacturing in 2026 is mostly a cost program that also cuts emissions. Energy, scrap and packaging are line items a plant can measure, so they are where most sustainability work starts.
The US Environmental Protection Agency defines sustainable manufacturing as making products through economically sound processes that minimize environmental impacts. Those processes also conserve energy and natural resources, so cost and resources sit in the same budget line.
Energy monitoring at the line or machine level is the usual first step. A plant that meters only at the building level cannot tell whether a compressor leak or an idle oven drives the bill. With sub-metering, a team can find machines that draw power between shifts and set shutdown rules for them.
Outside programs can also set the pace. Manufacturing partners in the Department of Energy’s Better Plants program pledge to cut energy intensity across their US operations by 25% over ten years.
Scrap reduction works the same way. Every scrapped part carries its material, energy and labor cost, so the quality models from trend 1 also cut waste. Circular models then extend the idea past the plant through remanufacturing, take-back programs and recycled inputs.
Many manufacturers are also changing how they power their sites and ship their goods.
For instance, solar power, green hydrogen, and carbon capture are gradually becoming key elements of their energy strategies. Reducing our environmental impact industrial companies are highly interested in creating sustainable packaging.
Packaging is a sensible place to begin, because its material, weight and waste are easy to measure. Track energy per unit produced and scrap rate by line as the first KPIs.
7. Additive Manufacturing and Mass Customization
Additive manufacturing, often called 3D printing, builds parts layer by layer from a digital file instead of cutting or molding them. In most plants its first job is not the final product but the tools and spares around it.
For example, jigs, fixtures and gripper fingers are the usual starting point. A maintenance team that waits weeks for a machined fixture can often print one in-house much sooner. The same applies to spare parts for older equipment whose supplier no longer makes them.
After that come short production runs and customized products. When each order differs slightly, printing avoids building a new mold for every variant. Advanced materials, such as high-performance polymers and metal powders, also keep widening the range of parts that can be printed.
Its data needs are modest, mostly CAD files and a list of slow-moving spares. Additive work can therefore start in a plant whose sensor data is not ready yet. Lead time for tooling and spare parts is the first KPI to watch.
8. Servitization: Connected Products and Aftermarket Services
Servitization means selling outcomes and services around a product, not just the product itself. An equipment maker might sell uptime, maintenance plans or usage-based pricing alongside the machine.
The enabling asset is installed-base data. Connected products report their hours, faults and wear from the customer’s site. With that data, a compressor maker can schedule service before a failure and price a contract on real usage. It can also spot customers who are about to switch brands.
Deloitte’s 2026 outlook expects agentic AI to reach aftermarket services as well, for example by ordering parts, reallocating inventory and scheduling service visits. That works only when product, service and customer records connect, which brings the story back to trend 2. Service revenue as a share of total revenue is a sensible first KPI.
Talk to Kanerika
Not Sure Which Trend Fits Your Plant?
Kanerika reviews your plant problems and data sources with your team, then recommends the first project and the KPI that will prove it within 90 days.
Schedule a Demo →Which Manufacturing Trends Should You Fund First?
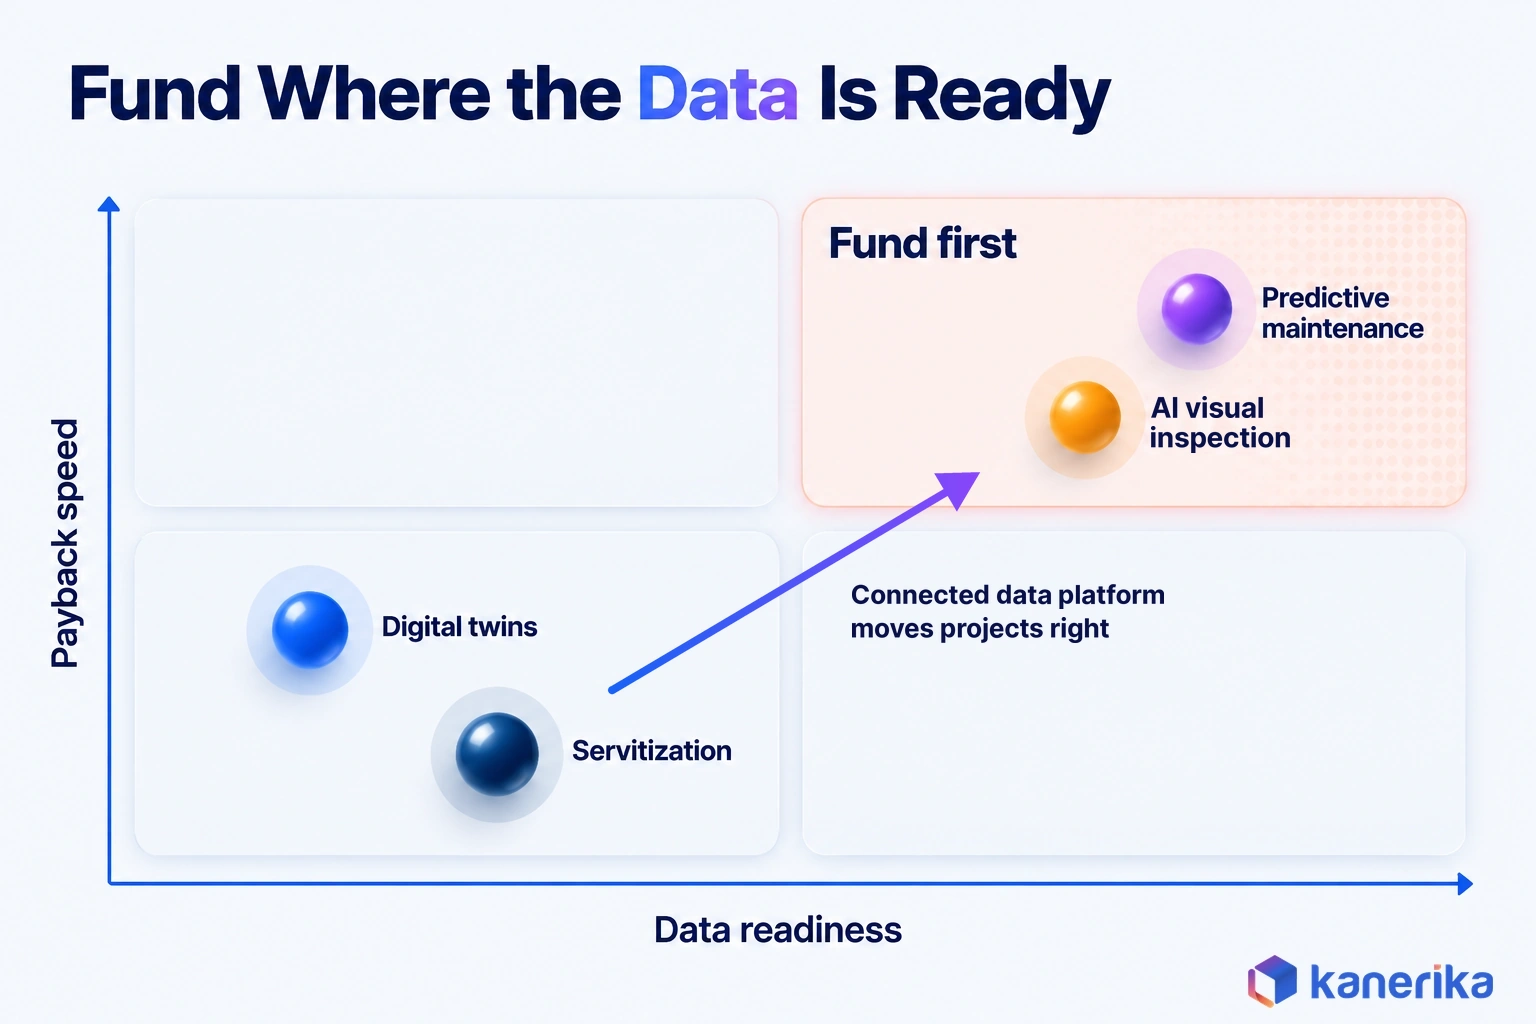
Among all the manufacturing industry trends, the one to fund first solves your most expensive plant problem with data you already collect. That rule sounds simple, yet budgets often go wrong here, because teams pick the most visible technology instead of the most ready one.
Two questions settle most choices. First, is the data for this use case already captured and trusted? Second, does the plant already measure the KPI the project would move? When both answers are yes, a pilot can prove value in about 90 days. When the data is missing, however, the first project is the data foundation itself.
The table below maps common plant problems to a first investment.
| Plant problem | First investment | Data prerequisite | 90-day pilot KPI |
|---|---|---|---|
| Frequent unplanned stops on a bottleneck asset | Predictive maintenance | Sensor history and past work orders | Unplanned downtime hours on that asset |
| High scrap or customer complaints | AI visual inspection | Labeled images of good and defective parts | First-pass yield |
| Reports take days and disagree | Connected factory data platform | Access to historian, MES and ERP data | Time to publish the weekly plant report |
| Missed deliveries from supplier delays | Risk mapping and demand sensing | Lead-time, supplier and order history | On-time delivery by supplier |
| Rising energy bills | Sub-metering and energy analytics | Line-level meter data | Energy per unit produced |
| Hard-to-fill repetitive roles | Cobots or AMRs | Cycle times and station layouts | Units per labor hour |
| Slow onboarding of new staff | Digital work instructions and copilots | Current SOPs and manuals | Time to competency |
The first three rows are the most common starting points, and the third row is often the precondition for the first two. So if your reports still take days, the platform row is your answer, and the AI rows follow once it is live.
When to hold a project back
Three signals say a project should wait. If nobody owns the KPI, or the data sits in a system you cannot reach, fix that before buying any tool. If the payback from the ROI steps below runs past your finance team’s limit, shrink the pilot to one asset or one line.
Starting priorities by industry segment
Industry segment shifts the starting point as well, because each segment feels a different pressure first. The table below shows where that pressure usually points, and our guide to data analytics in pharma goes deeper on one segment.
| Segment | Main pressure | Starting priority |
|---|---|---|
| Automotive | Tariffs on components and frequent model changeovers | Supplier risk mapping and AI inspection |
| Food and beverage | Food safety, short shelf life and energy use | Connected quality data and energy monitoring |
| Pharma | Batch records and regulatory compliance | Connected batch data and quality analytics |
| Electronics | Component shortages and fast product cycles | Demand sensing and AI inspection |
| Industrial equipment | Flat equipment margins and aftermarket competition | Installed-base data for servitization |
| Chemicals | Energy intensity and process safety | Process data platform and predictive maintenance |
Worked example: a three-plant manufacturer picks its first project
Consider a maker of industrial pumps with three plants. Leadership has budget for one project and three proposals. On the table are predictive maintenance on a bottleneck casting line, AI inspection on final assembly, and a plant-wide digital twin.
The team scores each option on data readiness and payback. The casting line already has vibration sensors and two years of work orders, and each stop there delays assembly in all three plants. Final assembly has cameras but no labeled defect images. The digital twin would need the MES and ERP connected first, which has not happened yet.
So predictive maintenance on the casting line goes first, with unplanned downtime hours as the 90-day KPI. Image labeling for inspection starts in parallel at low cost, while the twin waits for the data platform. The choice came from readiness, not from which idea sounded most advanced.
AI Assessment
How Ready Is Your Plant for AI?
Score your data, skills, governance and use-case readiness in a few minutes, and see which AI projects your plant can support now.
Start Your AI Assessment →How to estimate ROI before the pilot
A pilot needs a business case that finance accepts before it starts. Keep the math simple and use your own plant numbers:
- Record a baseline for the KPI over at least four weeks, such as downtime hours on one asset.
- Put a dollar value on one unit of the KPI, for example the margin lost per hour of downtime.
- Add up setup, integration and run costs for the pilot and its first year at scale.
- Measure the KPI change during the pilot against your own baseline, not against a vendor benchmark.
- Divide the total cost by the yearly value of that change to get the payback period.
Here is an illustrative example with assumed numbers. A press loses 10 hours a month to unplanned stops, and each hour costs $5,000 in lost margin, so the yearly exposure is $600,000. A pilot that removes 30 of those 120 hours is worth $150,000 a year. Against a total cost of $100,000, the payback is eight months.
Risks That Stall Manufacturing Technology Programs
Manufacturing technology programs usually stall on basics rather than on the technology itself. Security gaps, poor data and unclear ownership stop more projects than weak models do.
Security comes first, because connecting OT systems also exposes them. IBM’s X-Force Threat Intelligence Index 2026 ranked manufacturing the most attacked industry for the fifth year in a row. The sector drew 27.7% of incidents in 2025. Every new link between the floor and the cloud needs to be designed with that in mind.
Five risks show up again and again, starting with security:
- OT security exposure, when machines are connected without network segmentation or monitoring.
- Poor data quality, such as missing timestamps, inconsistent part numbers or untagged downtime.
- Pilot sprawl, where a dozen small pilots run with no path to production.
- Unclear ownership, when IT, OT and operations each assume another team owns the model.
- Thin on-site skills, when nobody at the plant can maintain the system after the vendor leaves.
A short governance checklist keeps these risks in check. NIST SP 800-82 Rev. 3, the Guide to Operational Technology Security published in September 2023, is the main US government guidance for securing it. NIST announced an initial public draft of Rev. 4 on September 21, 2026, with comments due November 30.
- Keep an inventory of every connected asset and its owner.
- Segment OT networks from business networks and control remote access, using the ISA/IEC 62443 series for control system security as the reference.
- Define each KPI and data field once, with a named data owner. Our guide to data governance challenges covers the common gaps.
- Set a stop-or-scale decision date for every pilot.
- Log model recommendations and operator overrides for review.
How Kanerika Helps Manufacturers Act on These Trends
Kanerika works data foundation first, then AI. Most of the manufacturing industry trends above depend on connected plant and business data. So engagements start with data integration across historian, MES and ERP systems.
FoodPharma, for example, shows the pattern. Its data was spread across six systems, more than 50 tables and about 1 TB of history. Kanerika consolidated it on Microsoft Fabric, and cross-functional reporting dropped from two business days to about 90 minutes. The team also recovered roughly 15 hours a week of manual BI work, as the FoodPharma case study and the Microsoft customer story describe.
AI comes next, once the data holds. For ABX, Kanerika’s AI-driven forecasting reached 85% accurate sales forecasts, as the ABX case study explains.
Kanerika is a Microsoft Solutions Partner for Data and AI, a Microsoft Fabric Featured Partner and a Databricks consulting partner. Its AI for manufacturing practice applies the same data-first sequence to plant use cases, and the manufacturing industry page gives more context.
Case Study
Reporting From Two Days to 90 Minutes With Microsoft Fabric
Kanerika consolidated FoodPharma’s data from six systems on Microsoft Fabric, cutting cross-functional reporting from two business days to about 90 minutes and recovering roughly 15 hours a week of manual BI work.
Read the Case Study →What Manufacturing Leaders Should Do in the Next 90 Days
The next 90 days should produce one funded pilot with a measured baseline, not a long strategy deck. The steps below turn this guide into four concrete deliverables.
- Weeks 1 to 2: list your three most expensive plant problems and the KPI each one moves. Deliverable: a one-page problem list with current KPI values.
- Weeks 3 to 4: audit the data behind each problem, including where it lives and who owns it. Our AI readiness assessment framework shows one way to score it. Deliverable: a data readiness score for each problem.
- Weeks 5 to 8: choose one project with the fund-first table and record its baseline. Deliverable: a signed business case with cost, KPI target and a stop-or-scale date.
- Weeks 9 to 12: run the pilot on one line or asset and review results weekly. Deliverable: a measured KPI change and a decision to scale, adjust or stop.
The plant from the opening scene would start with connected reporting, because its numbers do not yet agree. A plant with clean sensor and quality data would start with predictive maintenance or AI inspection instead. Either way, the rule is the same for every trend in this guide: fund first the one your data can already support.
Frequently Asked Questions
What are the manufacturing industry trends in 2026?
The main manufacturing industry trends in 2026 are industrial AI, connected factory data, flexible automation, supply chain resilience, workforce transformation, energy and circular production, additive manufacturing and servitization. Most plants get the fastest return from connected data and industrial AI, since the other six shifts depend on the same plant and business data being joined and trusted.
What are the smart manufacturing trends in 2026?
Smart manufacturing in 2026 centers on AI running inside daily plant work, IT/OT convergence, digital twins used for planning and early agentic AI. Deloitte’s 2025 survey found that 78% of large US manufacturers put more than 20% of their improvement budget into smart manufacturing, with reported gains of up to 20% in production output.
What is the next big thing in manufacturing?
Agentic AI and physical AI are the strongest candidates. AI agents can plan, schedule and sort service requests within set limits, and physical AI gives robots the ability to perceive and adapt. A Manufacturing Leadership Council survey cited by Deloitte found that 22% of manufacturers plan to use physical AI within two years, up from 9%.
What is the difference between Industry 4.0 and Industry 5.0?
Industry 4.0 describes connected, data-driven production built on sensors, automation, cloud platforms and analytics. Industry 5.0 adds three goals on top of that technology base, namely human-centric work, sustainability and resilience. Most plants treat Industry 5.0 as a guide for how they apply Industry 4.0 tools, with people kept in charge of final decisions.
How are robots changing manufacturing jobs?
Robots take over repetitive, heavy or hazardous tasks such as machine tending and palletizing, and people shift toward setup, maintenance, quality and problem solving. The IFR counted 542,000 industrial robots installed in 2024, and Deloitte still expects more than 81% of task hours to stay human-driven. Training workers to run automation is the main change.
How can manufacturers reduce production downtime using AI?
Start with predictive maintenance on the two or three assets whose failure stops the whole line. Combine sensor data, such as vibration and temperature, with past work orders so the model learns which patterns precede real failures. Send alerts into the maintenance workflow, record each outcome and track unplanned downtime hours against a baseline over 90 days.
How can small and mid-sized manufacturers adopt Industry 4.0?
Small and mid-sized manufacturers should start with one costly problem and one KPI instead of a plant-wide program. Connect the data that problem needs, often a historian, the ERP and quality records, then run a 90-day pilot on one line. Cloud data platforms and off-the-shelf sensors keep entry costs low, and a successful pilot funds the next step.
Which manufacturing trend should a company invest in first?
Invest first in the trend that solves your most expensive plant problem with data you already collect and a KPI you already measure. For most plants that means connected factory data or predictive maintenance. Estimate ROI from your own baseline, setup and run costs, then prove the result in a 90-day pilot before scaling it to other lines.
What are the emerging and advanced technologies in manufacturing?
The leading technologies are predictive maintenance, AI visual inspection, generative AI copilots, AI agents, digital twins, collaborative robots, autonomous mobile robots, physical AI, additive manufacturing and connected products. Each one needs a specific data source, such as sensor history, labeled defect images or installed-base data, so plants should check data readiness before choosing what to fund.
Is the manufacturing industry declining in 2026?
The data shows an industry under cost pressure that keeps investing. In the NAM Q2 2026 survey, 74.2% of manufacturers felt positive about their own company’s outlook, slightly down from 75.3% in the first quarter. Raw material costs and trade uncertainty were the top challenges, and Deloitte links new investment to incentives, data centers and semiconductors.
What are the biggest challenges facing manufacturers in 2026?
Raw material costs and trade uncertainty lead the list, cited by 83.1% and 71.8% of respondents in the NAM Q2 2026 survey. Manufacturers also face a skills gap, with up to 1.9 million jobs that could go unfilled by 2033, and frequent cyberattacks, since IBM ranks manufacturing the most attacked industry for the fifth year running.
Which manufacturing sectors are growing?
Deloitte’s 2026 manufacturing outlook ties much of the new investment to semiconductors, the supply chains behind data center build-outs and projects supported by federal incentives. According to Deloitte, the advanced manufacturing investment credit also rose from 25% to 35%. Manufacturers that supply these projects with equipment, components and materials stand to gain the most from that spending.
How is AI changing the manufacturing industry?
AI is moving from pilots into daily plant work. Predictive maintenance flags failures before a line stops, visual inspection catches defects at line speed, and copilots help technicians find past fixes in manuals and work orders. AI agents are starting to handle planning tasks within set limits. Each use depends on clean, connected plant data that teams trust.
What is green manufacturing?
Green manufacturing means producing goods with less energy, material and waste across the whole product life. In practice it starts with measurable steps, such as machine-level energy monitoring, scrap reduction, recycled inputs and lighter packaging. Circular models extend it through remanufacturing and take-back programs, which keep products and materials in use for longer.
How are smart factories changing manufacturing?
Smart factories connect machine, quality, MES and ERP data into one model, so teams see problems within a shift instead of a week later. That shared data also powers digital twins, which let planners test a new product mix or line layout virtually before changing the real line. Decisions become faster and much easier to check.
What are the 5 KPIs for manufacturing?
Five widely used manufacturing KPIs are overall equipment effectiveness (OEE), throughput, first-pass yield, unplanned downtime and on-time delivery. OEE combines availability, performance and quality into one score. Throughput counts units produced per period. First-pass yield shows the share made right the first time, and on-time delivery tracks orders shipped by the promised date.